Shanxi Jianing Forging can process large-diameter pressure vessel shell forgings made of carbon steel, stainless steel, and alloy steel. The station has a wealth of real-world cases of cylinder forging, fully demonstrating the forging capabilities of large-size cylinders and the corrosion-resistant results of finished products.
In the field of heavy hydraulic equipment manufacturing, cylinder forgings serve as core pressure-bearing components, and their quality directly affects the stability and safety of equipment operation. Recently, Jianing Forging undertook a cylinder forging project for a hydraulic heavy equipment factory in Jinhua, Zhejiang. Through targeted process optimization and full-process quality control, they successfully delivered forging products that meet stringent technical requirements.
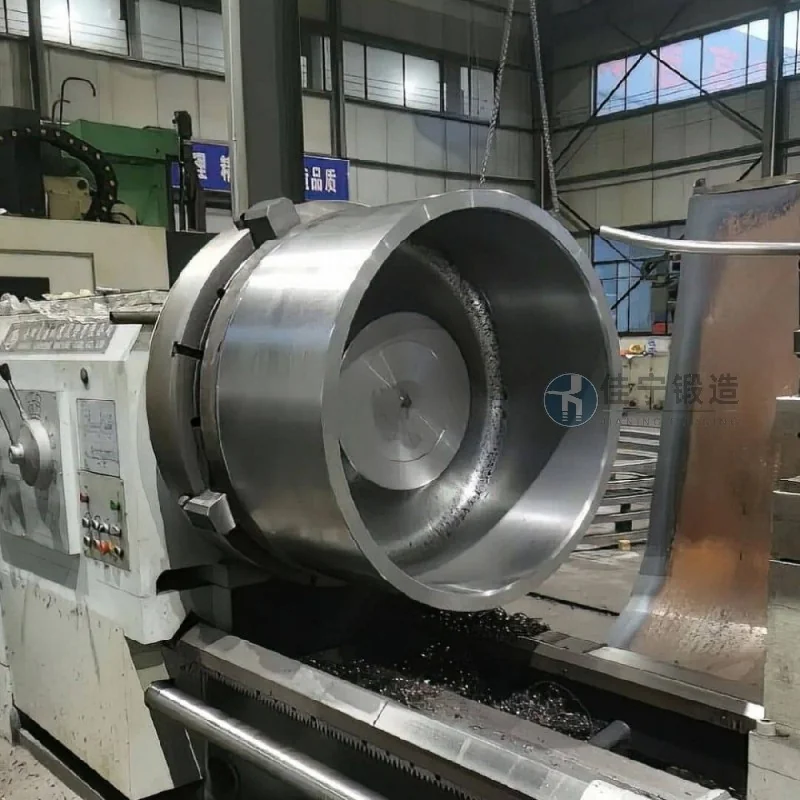
This hydraulic heavy factory has long been engaged in the production of large hydraulic cylinders and cylinder assemblies. Its shell forgings must withstand high-pressure, high-frequency alternating loads, and have high requirements for material density, dimensional accuracy, and surface finish. Jianing Forging is the supplier of this batch of cylinder forgings, undertaking the entire processing process from raw materials to finished products.
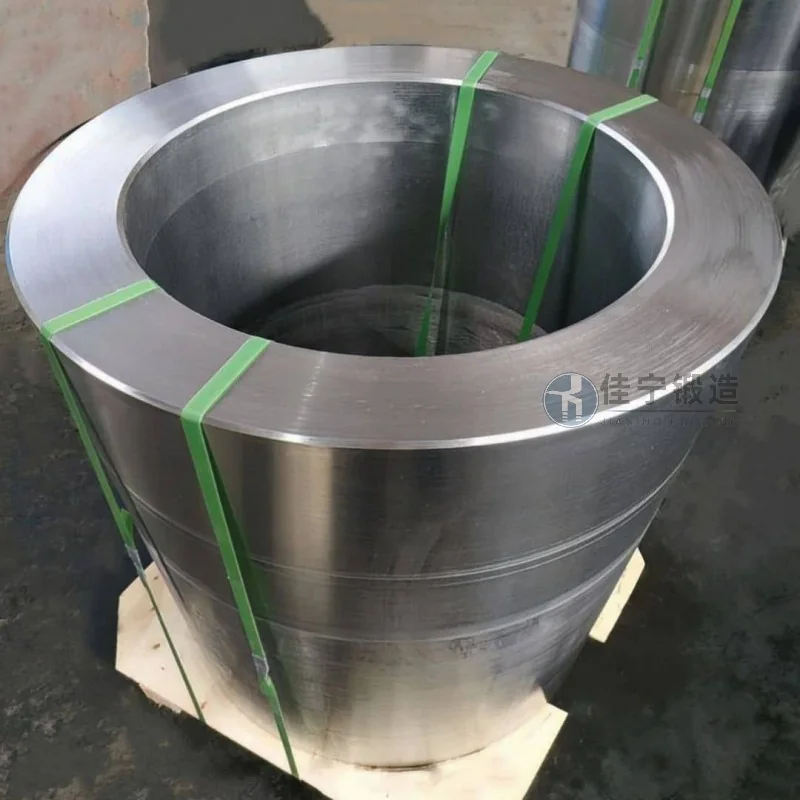
At the early stage of the project, the customer faced three key challenges: First, the cylinder forgings had a diameter exceeding 1.2 meters, uneven wall thickness, and conventional forging processes easily caused metal flow disorder; second, the client's internal technical specifications required that there must be no single defect exceeding 1mm inside the forging, and ultrasonic testing was required; third, delivery times were tight, and traditional forging solutions could not meet both quality and efficiency requirements. In addition, customers set high standards for controlling heat treatment deformation of forgings to avoid insufficient machining allowance in subsequent processing.
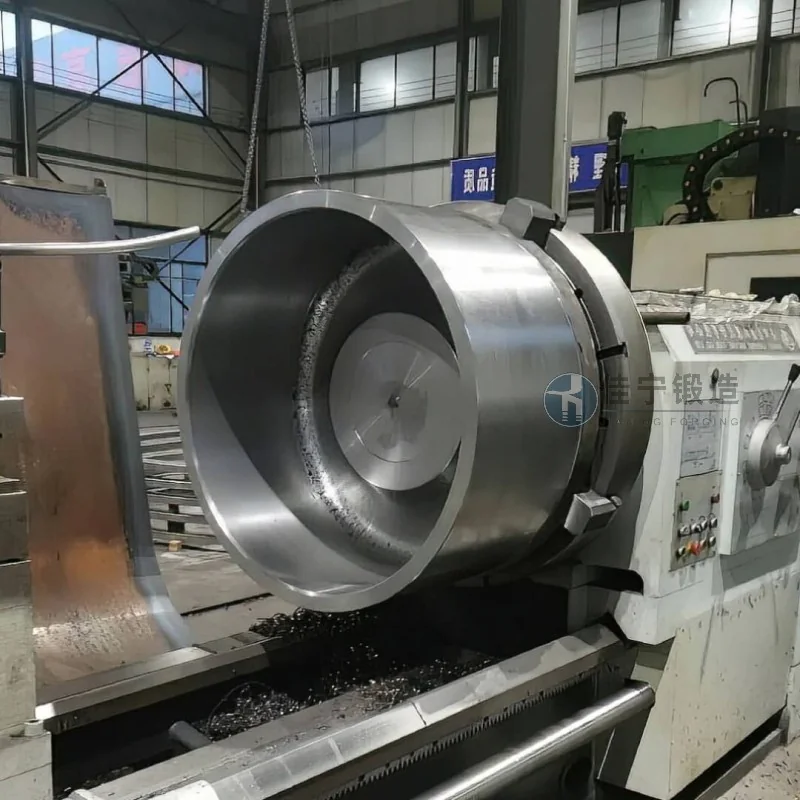
To address these pain points, Jianing Forging has implemented multiple targeted measures:
Optimized forging ratio and deformation process—through multiple upsetting and drawing processes, metal flow lines are evenly distributed along the cylinder axis, eliminating coarse structure;
Relatively accurate control of heating and cooling parameters—using segmented heating and isothermal annealing processes to reduce internal stress and minimize heat treatment deformation;
Full-process nondestructive testing coverage—from blanks to semi-finished products, ultrasonic flaw detection and magnetic particle inspection are performed piece by piece, helping internal and surface defect rates stay below customer standards;
Shortening process connection time — through quick mold changeover and standardized tooling, the production cycle for individual parts is shortened by about 20%, meeting customer delivery deadlines.
Ultimately, the delivered cylinder forgings were inspected by the customer third-party and all indicators met the requirements, passing acceptance on the first try. This collaboration validates Jianing Forging's process responsiveness and quality support level in the field of large special-shaped forgings.

